
 English
 中文简体
How Transformer Varnish Impregnation Affects Lifespan and Reliability in Service
2026-09-18
Content
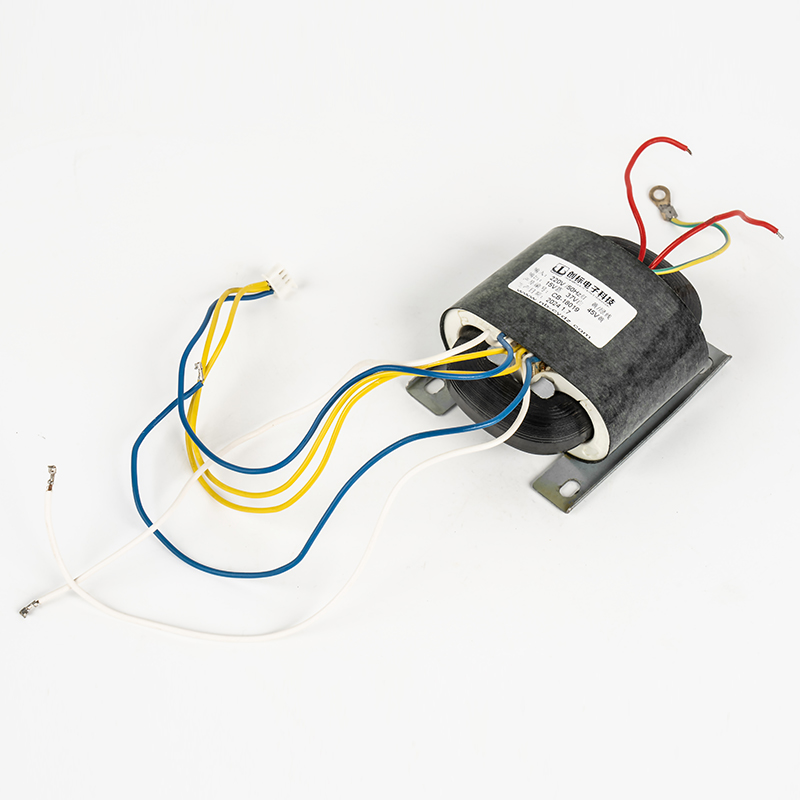
A low-voltage control transformer was returned to the workshop after only three years of service. The customer reported charred winding insulation and intermittent output. When the production record was reviewed, the impregnation step had been skipped to save time. That short-cut turned a transformer that should have served for decades into a scrap pile.
Transformer varnish impregnation is not a cosmetic finishing step. It controls moisture, insulation, mechanical rigidity, and heat transfer inside the winding. In short, the way a transformer is varnish-impregnated is one of the strongest influences on how long the transformer will last in service.
Why Varnish Impregnation Is the Lifespan Lever in Wound Components
The windings of a transformer are never perfectly solid. Between copper turns, between layers, and between the coil and the bobbin, tiny air pockets always exist. Those pockets become weak points under electrical stress and mechanical vibration.
- Electrical stress: Air in voids ionizes under voltage, causing partial discharges that erode enamel insulation over time.
- Mechanical stress: Unbonded turns vibrate at line frequency or switching frequency, eventually wearing through the insulation.
- Moisture and contamination: Air pockets absorb moisture and pollutants, which lowers insulation resistance and encourages corrosion.
- Thermal stress: Air conducts heat poorly. Varnish, even in thin layers, conducts heat better and helps reduce the hot-spot temperature.
The practical result is a well-known thermal relationship: for every 10 °C reduction in hot-spot temperature, the expected life of a typical insulation system can roughly double. Impregnation does not change the physics of the copper or core, but it changes the temperature and the environment around them.
Relative insulation life decreases as winding hot-spot temperature rises
Well-Impregnated vs. Poorly Impregnated: What Changes in Practice
The differences are not subtle. A transformer with complete varnish penetration behaves differently from one with only surface coverage. The table below summarizes the long-term effects seen in service.
| Aspect | Well-impregnated | Poorly impregnated or skipped |
|---|---|---|
| Insulation resistance | Stable, high even after humid weeks | Drops noticeably with humidity |
| Mechanical integrity | Coils move as a solid block | Loose turns under load and vibration |
| Moisture ingress | Blocked by filled gaps | Capillary paths reach into winding |
| Hot-spot temperature | Lower because heat conducts through varnish and core | Higher because air is trapped |
| Expected service life | Full design life, often 15–25 years | Premature failure within a few years |
Process Variables That Decide Long-Term Performance
Once a varnish has been selected, the process decisions are just as important as the chemistry.
Vacuum Impregnation vs. Conventional Dipping
Conventional dipping lets varnish cover the outer surface, but capillary action may not push resin into the deepest interlayer spaces. Vacuum impregnation removes air and moisture from the winding before resin is introduced under pressure, so the varnish reaches the narrow gaps inside the coil. For power, high-frequency, automotive, medical, and industrial transformers, vacuum impregnation is strongly preferred.
Varnish Chemistry and Insulation Class
Varnishes are classified by their maximum continuous hot-spot temperature. A common mistake is using a lower-class varnish in a high-temperature design; the resin ages much faster and becomes brittle, exposing the winding to moisture and vibration damage.
| Insulation class | Maximum hot-spot temperature | Typical use |
|---|---|---|
| A | 105 °C | Low-cost, low-temperature applications |
| E | 120 °C | General-purpose industrial transformers |
| B | 130 °C | Common in power and audio transformers |
| F | 155 °C | Higher-load equipment, motors, drives |
| H | 180 °C | Harsh environments and high-temperature designs |
Drying and Curing
Baking-type varnishes require a controlled time-temperature profile. If curing is incomplete, the resin stays soft and has lower dielectric strength. If the temperature is too high, the varnish can cure too quickly on the outside and trap solvent inside, creating new voids. Self-drying varnishes are used for small batches, but they generally provide less penetration and lower mechanical strength.
Verification and Quality Testing
The process is not finished until the treated winding is electrically verified. Insulation resistance, hi-pot testing, and visual cross-section checks on sacrificial samples all help confirm that the varnish reached the inner layers rather than just forming a shiny shell.
What to Look For When Ordering Impregnated Transformers
When you evaluate a transformer supplier, the impregnation line should be near the top of the checklist. Ask whether they use vacuum pressure impregnation, what varnish class they standardize on, and how they verify the cure.
A reliable transformer manufacturer will usually share its process documents and test records with you. For custom transformer requirements, the impregnation specification should be written into the same document as the electrical specifications.
Five Questions to Ask Before Placing an Order
- What varnish insulation class (B, F, or H) is used on this model?
- Is the entire coil vacuum impregnated or only dipped in varnish?
- What is the target varnish pick-up by weight, and how is it measured?
- Are all units high-pot and insulation-resistance tested after curing?
- Can the supplier show cross-section samples that prove the inner layers are filled?
Frequently Asked Questions
Can varnish impregnation repair damaged magnet wire?
No. Varnish can fill small pinholes and reduce the impact of minor scratches, but it cannot replace damaged enamel consistently. Proper wire handling and layer insulation must come first.
Does more varnish mean a longer transformer life?
Not necessarily. Excessive varnish can crack under thermal cycling, and trapped solvent from an incorrect curing cycle creates new voids. The goal is complete, uniform filling with a correctly cured resin.
Is vacuum impregnation always required?
For small, low-stress signal transformers, controlled dipping may be sufficient. For power, high-frequency, automotive, medical, or industrial transformers, vacuum impregnation is strongly recommended because it removes air and moisture before filling the voids.
How can we verify impregnation quality after delivery?
Measure insulation resistance before and after humidity exposure, inspect cross sections of sacrificial samples, and check the unit for abnormal hum or resonance under load.
Transformer varnish impregnation is a quiet process, but its consequences are loud. A deep, well-cured vacuum impregnation cycle seals the winding against insulation-killing conditions and keeps the hot-spot temperature lower. A skipped or rushed process leaves hidden voids that turn into partial discharge, vibration wear, moisture absorption, and early failure. When you specify or buy a transformer, make the impregnation process part of the acceptance criteria. It is one of the most direct and measurable ways to extend transformer lifespan.
Welcome To CHUANGBIAO
Address : No.420-3, Sanbei East Road, Guanhaiwei Industrial Zone, Cixi City, Ningbo, Zhejiang, China
Contact
- Tel: +86 186 6825 0703
- Email: linjian@nbcbdz.com
About us
Products
Copyright © Ningbo Chuangbiao Electronic Technology Co., Ltd.
All Rights Reserved. EI Transformer Manufacturer


